If you’ve ever walked through a precision machining shop, watched a Horizontal Surface Grinder transform raw metal stock into a flat, consistent part, you’ve probably noticed a curious component sitting dead-center on the machine’s worktable: the magnetic chuck. As a supplier of Horizontal Surface Grinders, I’ve spoken to countless machinists, quality managers, and novice operators who either take this part for granted, underestimate its impact on their work, or even misunderstand how it works. Today, I want to break down exactly what the magnetic chuck does on a Horizontal Surface Grinder, why it’s the unsung hero of surface grinding, and why picking the right one for your machine is non-negotiable for both quality and efficiency. Horizontal Surface Grinder
Let’s start with the basics. A Horizontal Surface Grinder uses a rotating abrasive wheel (mounted on a horizontal spindle) to shave tiny, uniform layers of material from a workpiece, resulting in a surface so flat it’s often measured in microns—one-millionth of a meter. The entire process relies on holding that workpiece rock-solid, perfectly aligned, and free from shifting during cuts. That’s where the magnetic chuck comes in. Unlike mechanical clamps, vises, or fixtures that add weight, take up workspace, and can distort thin or delicate parts, the magnetic chuck holds the workpiece evenly across its entire surface using controlled magnetic force. It’s not just a holding tool; it’s the foundation that makes every precision cut possible.
First, let’s get into how it works, because that’s where most new operators get tripped up. Most horizontal surface grinder magnetic chucks are either permanent or electro-permanent. A permanent chuck uses a grid of alternating north and south pole magnets arranged under its steel working surface. When you engage the chuck, you rotate a control lever that aligns the internal magnets, creating a continuous magnetic field that extends up through the chuck’s top, through the workpiece, and back down into the chuck’s steel body. The steel workpiece acts as a magnetic bridge, so the force pulls it tight to the chuck—no gaps, no slippage. Electro-permanent chucks add an extra layer: they use a short electric pulse to adjust the magnetic field, rather than running power continuously, which makes them more energy-efficient and eliminates the risk of power loss mid-job that would make a standard electro-magnetic chuck drop a workpiece mid-cut.
The role of the magnetic chuck isn’t just “holding the part.” Let’s break that down into three specific, non-negotiable functions that directly impact your end product. First, it ensures perfect flatness and alignment. When you clamp a part with a vise, even a precision machined vise, you’re applying pressure at discrete points along the edge of the part. If the part is thin—say, a 1/8-inch steel shim or a small mold insert that’s only a few millimeters thick—that edge pressure can cause the part to bow or twist. Once you release the vise after grinding, the part springs back to its original shape, leaving you with a surface that’s not flat. A magnetic chuck applies uniform force across the entire bottom surface of the part. There’s no edge pressure, so even thin, flexible parts stay flat during the entire grinding process. I’ve seen this make or break a job more times than I can count: a customer brought in a set of 50 thin stainless steel spacers that came out warped when using a vise, switched to our grinder’s magnetic chuck, and every single one came within 0.001mm of flatness. That’s not a coincidence—that’s the magnetic chuck doing its job.
Second, it maximizes efficiency for both small and large production runs. Think about how long it takes to set up a part in a vise: you have to tighten each bolt, check for runout, adjust for alignment, and make sure there’s no gap between the part and the vise jaw. For a production run of 100 identical parts, that setup time adds up fast. A magnetic chuck? You just wipe the chuck surface clean, lay the part down, engage the lever, and you’re ready to grind in 10 seconds or less. Even for multiple small parts, you can fit them all on the chuck at once, grinding them in a single pass instead of one at a time. Last quarter, a customer who makes custom automotive gaskets told us that switching to our horizontal surface grinder with a high-pull magnetic chuck cut their setup time per batch by 70% and increased their daily output by 35%. That’s real, bottom-line impact from a component most people don’t even list on their parts sheet.
Third, it expands the types of materials you can work with. Magnetic chucks only work on ferrous metals—steel, iron, some stainless steels—so you might be thinking, “That’s a downside.” But here’s the thing: most high-precision surface grinding jobs are on ferrous materials, because those are the ones used for tooling, molds, machinery parts, and structural components that need tight tolerances. Even if you do work with non-ferrous materials like aluminum, brass, or copper, you can use a custom magnetic chuck setup, like a sub-plate with a thin steel base that attaches to the chuck, so you can still hold those parts securely without having to clamp every single one. That versatility means your horizontal surface grinder is a more flexible machine, able to handle both ferrous production runs and one-off non-ferrous jobs without investing in extra clamping equipment.
But here’s where many shops make a critical mistake: not all magnetic chucks are created equal, and picking the wrong one can ruin even the best horizontal surface grinder job. Let’s talk about the key specifications that matter, because this is what I emphasize to every customer when they’re ordering a grinder from us. First is pull force. That’s how much magnetic force the chuck can exert, measured in psi. If you’re grinding a thick, heavy steel block, you need a high-pull force chuck—often 100 psi or more—to make sure the part doesn’t shift even when the grinding wheel is applying tons of downward pressure. If you’re grinding thin, delicate parts, you don’t need that much pull force, but you do need consistent, uniform pull across the entire surface to avoid warping. Second is the pole pattern. The pole configuration—whether it’s fine-pole, standard-pole, or even variable-pole—determines how evenly the magnetic force is distributed. Fine poles are better for small parts or thin materials, because they create a denser magnetic field that holds small areas securely. Standard poles work for larger, thicker parts. Variable-pole chucks are great because you can adjust the pole strength for different jobs, so you can hold a tiny washer one minute and a 12-inch steel plate the next without switching chucks. Third is the surface finish of the chuck itself. If the chuck’s top surface is pitted, scratched, or uneven, that creates tiny gaps between the chuck and your workpiece, even if you can’t see them. Those gaps let magnetic force slip, which can cause the part to shift. It also means your grinding wheel is contacting the chuck surface in spots, which dulls the wheel faster and can scratch the bottom of your workpiece. All our magnetic chucks come with a ground, precision-flat top surface that’s within 0.0002mm of flatness, so you get consistent contact every time.
I also want to address a common myth I hear all the time: “Magnetic chucks are only for light, rough grinding.” That couldn’t be further from the truth. Modern electro-permanent magnetic chucks are powerful enough for heavy-duty surface grinding, even on workpieces weighing hundreds of pounds. We recently delivered a horizontal surface grinder with a 16-inch magnetic chuck to a tool and die shop that was grinding large, thick steel mold bases for automotive body panels. Before, they were using a mechanical fixture that took 20 minutes to set up per part and left the surface with minor clamping marks. With the magnetic chuck, setup takes 2 minutes, and the flatness of the finished mold base is now within 0.0005mm—tight enough to hold up to millions of stamping cycles. The magnetic chuck didn’t just make their process faster; it improved the quality of their entire product line.
Another thing to consider is maintenance, which plays a big role in how long your magnetic chuck works and how consistent its performance stays. A good magnetic chuck will last for years, but only if you take care of it. The biggest mistake operators make is not cleaning the chuck surface between jobs. Metal shavings, coolant residue, and oil can build up on the chuck, creating gaps between the chuck and the workpiece that reduce pull force. Every time you finish a job, wipe the chuck with a clean, dry cloth—never use abrasive materials like steel wool, because that will scratch the surface. For deeper cleaning, use a mild degreaser, then dry it completely before your next job. Also, check the control lever periodically to make sure it’s aligned properly—if it’s not engaging fully, you’re not getting the full pull force of the chuck. We include a full maintenance guide with every grinder we sell, and our service team is always available to walk customers through routine checks, even years after their purchase.
Let’s also talk about a less obvious role of the magnetic chuck: safety. When you’re grinding at high speeds, a part that shifts mid-cut is a massive hazard. It can fly off the worktable, break the grinding wheel, or cause serious damage to the machine—and more importantly, to the operator. Magnetic chucks provide consistent, reliable holding force that’s far more consistent than a human tightening a clamp. I’ve had customers tell me horror stories of a vise bolt coming loose mid-grind, a part flying across the shop, and almost hitting someone. A properly selected and maintained magnetic chuck eliminates that risk entirely. That’s not a trivial benefit—safety should be at the top of every shop’s priority list.
If you’re still wondering how this all ties back to your horizontal surface grinder, let’s put it all together. The horizontal surface grinder’s job is to remove material evenly, create a flat, precise surface, and do it efficiently. The magnetic chuck is the component that makes every step of that process possible: it holds the part flat to eliminate distortion, it cuts setup time to maximize output, it expands the range of materials and parts you can work with, it improves surface quality, and it keeps your shop safe. It’s not a fancy, high-tech part that gets all the attention, but it’s the heart of your surface grinding operation.
At the end of the day, choosing the right magnetic chuck for your horizontal surface grinder isn’t a small decision. It’s the difference between mediocre parts that get rejected and parts that meet strict tolerances, jobs that take all day and jobs that get done in half the time, and a shop that runs smoothly and one that’s constantly dealing with delays and rework. If you’re looking to upgrade your horizontal surface grinder, or if you’re tired of wasting time on setup and rework because of a bad magnetic chuck, let’s talk. We’ve helped hundreds of shops match their grinder to the perfect magnetic chuck for their specific needs, from small job shops making custom parts to large production facilities running 24/7. We’ll walk you through pull force, pole patterns, maintenance, and every other detail to make sure you get a setup that works for you, not against you.
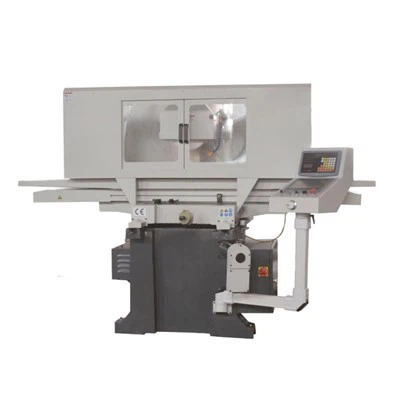
If you’re ready to stop settling for good enough and start getting consistent, high-quality results from every surface grind, don’t hesitate to reach out for a consultation. We’re here to help you build a setup that makes your work easier and your products better.
Precision Centerless Grinder References
- Todd, R. H., Allen, D. K., & Alting, L. (1994). Manufacturing Processes Reference Guide. Industrial Press Inc.
- Kalpakjian, S., & Schmid, S. R. (2014). Manufacturing Engineering and Technology (7th ed.). Pearson.
- Shaw, M. C. (1996). Principles of Abrasive Processing. Oxford University Press.
- HMT Limited. (2008). Surface Grinding Technology. Tata McGraw-Hill Education.
- American Society of Mechanical Engineers. (2019). B5.57-2019: Surface Grinders – Safety Requirements. ASME International.
Wuxi Mingxu Machinery Equipment Co., Ltd.
As one of the most professional horizontal surface grinder manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy the best horizontal surface grinder for sale here from our factory. Also, custom service is available.
Address: No. 5-5 Jinke Wealth Plaza, Changjiang North Road, Xinwu District, Wuxi City, Jiangsu Province
E-mail: yingyingmxjd@163.com
WebSite: https://www.mingxu-china.com/
